
Air Compressor Maintenance: From Reactive to Proactive
Release time:
2025-10-22
Building a Preventive Maintenance System: From Reactive Repairs to Proactive Management
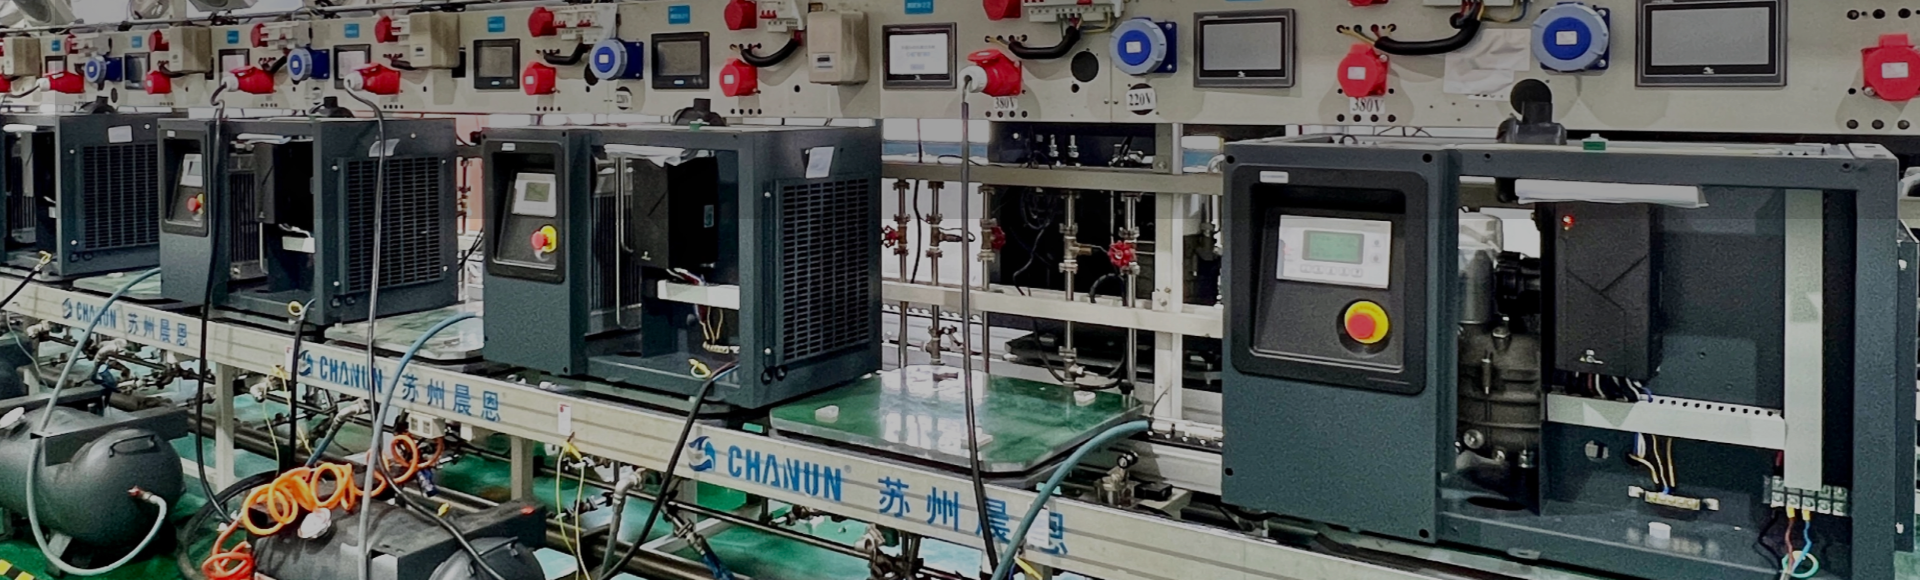
CHANUN air compressor
Transform equipment management so your company moves from a “fire brigade” to a “prevention station.”
In industrial production, unplanned equipment downtime often causes sudden, severe losses. The traditional “fix it when it breaks” approach not only disrupts production schedules but keeps maintenance staff constantly firefighting. Shifting from reactive repairs to proactive prevention has become a key competitive lever for enterprises.
01
Change the mindset: from “firefighting” to “fire prevention”
Equipment management has evolved significantly—from Breakdown Maintenance (BM) to Preventive Maintenance (PM). Breakdown maintenance is the most primitive mode: repairs occur only after a failure, causing long downtimes and large production losses. Preventive maintenance, by contrast, schedules regular inspections, servicing, and parts replacement based on time or cycles—achieving the first leap from “repair when broken” to “prevent breakage.”
More advanced philosophies include Reliability-Centered Maintenance (RCM) and Total Productive Maintenance (TPM). TPM advocates “everyone’s participation,” having operators take responsibility for routine upkeep and minor fault handling so maintenance teams can focus on specialized repairs and continuous improvement. The ultimate goal is to pursue “zero failures, zero defects, zero accidents.”
02
Equipment classification: the foundation for differentiated strategy
Resources are limited—treating all equipment the same is unaffordable. The first step in building a preventive maintenance system is scientific equipment classification. A common method is the ABC classification, which grades equipment according to its impact on production, quality, cost, and safety.
• Class A (critical equipment): use a combination of preventive and predictive maintenance and allocate top resources.
• Class B (important equipment): adopt standardized periodic maintenance.
• Class C (general equipment): use breakdown maintenance to save costs.
This differentiated strategy ensures optimal allocation of resources.
03
Core elements of preventive maintenance
A scheduled maintenance plan is the foundation of preventive maintenance. This includes daily inspections, weekly lubrication and cleaning, monthly performance tests and spare-parts replacement, etc. Creating a “health record” for each asset that documents lifecycle data is a crucial basis for predictive maintenance.
Inspection (point-check) systems are a key component. Implement a “dual-confirmation” inspection process to prevent cursory checks. Inspection items should be specific and standardized—for example, when checking drive belts, specify how to detect belt edge deviation and give concrete acceptance criteria such as “no more than 10% deviation.”
04
Predictive maintenance: the advanced form of preventive maintenance
Predictive Maintenance (PdM) is the advanced form of PM. It is condition-based and forecasts when failures are likely to occur by monitoring vibration, temperature, oil condition, and other parameters during operation, enabling “repair as needed.”
Techniques include vibration analysis, oil analysis, and infrared thermography. With the development of the Industrial Internet of Things (IIoT), predictive maintenance is becoming more precise and widespread. Companies can predict failures more accurately and automatically adjust maintenance schedules.
05
Total participation: the guarantee for system implementation
Successful implementation of a preventive maintenance system requires full participation. Establish a skill matrix to train maintenance technicians and operators systematically so everyone can fulfill their responsibilities.
Operators must master daily inspection skills and achieve the “four competencies”: be able to operate, maintain, diagnose, and handle minor faults. Maintenance technicians should master more advanced predictive techniques such as vibration analysis and infrared camera operation.
06
Data-driven: the basis for continuous improvement
Building a complete data collection and analysis system is the foundation for continuous optimization of the preventive maintenance program. Key metrics include Overall Equipment Effectiveness (OEE), Mean Time Between Failures (MTBF), and Mean Time To Repair (MTTR).
By analyzing trends in these metrics, you can identify weak points in equipment management and make targeted improvements. For example, if a machine’s OEE is only 65%—far below a world-class level of 85%—analysis may reveal the main loss is low performance rate (idle running and frequent small stops). That insight shifts the improvement focus from “repair” to “management.”
Building a preventive maintenance system marks a company’s shift from coarse management to fine-grained control. It begins with a fundamental change in leadership thinking and succeeds through a solidly constructed system that combines classification strategy, predictive technologies, lean spare-parts management, talent incentives, and data measurement. The returns on this transformation are substantial: lower operating costs, higher asset returns, more stable product quality, and more reliable delivery.
Start now—begin by evaluating one critical asset, drawing your first skill matrix, and calculating your first real OEE. Step by step, you’ll be on the path to excellent equipment management.
Related news


Service Hotline: 86 13862059949
CONTACT US
Address: No.58, Dongfu Road, Suzhou Industrial Park,Suzhou, jiangsu Province, China.
Tel: (+86) 0512-62529535
WhatsApp/Wechat: (+86) 13862059949
E-mail: jiaqi.wu@chanuncompressor.com
Copyright © CHANUN 2020 All rights reserved 苏ICP备08024400号-4
www.300.cn