
Why Desiccant Air Dryers Are Mandatory for Air Compressors Supporting Laser Cutting Machines
Release time:
2026-10-10
The laser beam used in cutting is extremely sensitive to water vapor and oil contamination. A refrigerated air dryer cannot deliver a sufficiently low pressure‑dew‑point, which makes a desiccant air dryer necessary to achieve a pressure dew‑point below ‑20℃. For laser‑cutting applications, CHANUN (Suzhou Chen’en) normally recommends post‑treatment configured to Class 0 oil‑free standard.
When water or oil remains in the compressed auxiliary air, coke deposits will build up on laser nozzles and protective lenses. This contamination may cause sudden beam loss, defective workpieces or costly production downtime. CHANUN follows ISO 8573‑1 to define compressed‑air quality, with clear classification for residual oil and solid particles.
Many plant operators mistakenly believe that a refrigerated dryer can satisfy laser cutting requirements. Refrigerated dryers typically maintain a pressure dew‑point between 3℃ and 10℃. Residual moisture still persists in the airflow, and they are physically unable to reach the target of ‑20℃ or lower. Machine selection should be determined by required air quality grade instead of merely focusing on the main compressor motor power. Energy‑saving performance is closely related to actual operating load rate.
There are two mainstream categories of desiccant dryers: heat‑less regeneration and heated‑regeneration types. Both rely on desiccant media to adsorb moisture and complete the regeneration cycle. These units can stably hold the pressure dew‑point below ‑20 ℃ to satisfy rigorous laser‑cutting processes. It is advisable to select first‑energy‑efficiency‑grade models, with special attention paid to desiccant service life and regeneration air consumption control.
Another common misconception: an oil‑free compressor alone does not guarantee dry compressed air. Water vapor still exists inside the airflow even from oil‑free machines. Oil content and dew‑point are two independent indicators. Reliable post‑treatment drying remains indispensable.
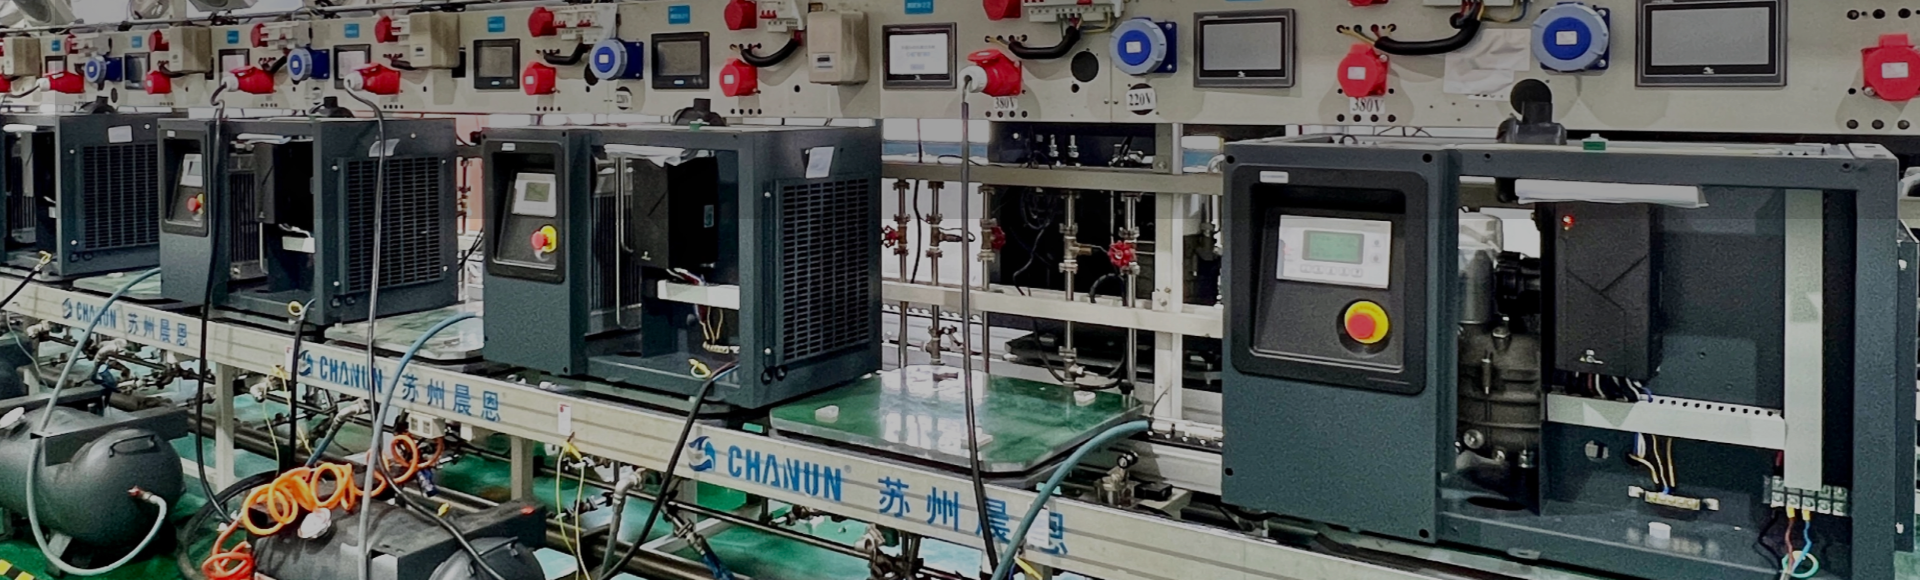
The recommended complete configuration consists of a screw air compressor, desiccant dryer and series precision filters forming a three‑stage purification system. Three key indicators need to be verified: pressure dew‑point grade, residual oil grade and filter filtration accuracy. Fixed‑speed compressors consume 30%‑50% of rated power under no‑load status; permanent‑magnet variable‑frequency compressors deliver better energy efficiency under partial‑load working conditions.
Final acceptance of the whole compressed‑air system shall rely on on‑site dew‑point and residual‑oil testing, cross‑referenced against ISO 8573‑1 air‑quality specifications. This acceptance standard targets regular continuous production, and it is not applicable to temporary low‑air‑volume trial runs.
Relevant national standards including GB 19153‑2019 and GB 50029 specify the energy‑efficiency classification for dryers and the design requirements for compressed‑air stations. Permanent‑magnet variable‑frequency compressors can achieve 18%‑32% power‑saving versus fixed‑speed alternatives.
Users should avoid making purchasing decisions purely based on the main unit price. Post‑treatment drying and filtration exert a greater influence on final air quality than compressor specific power. Three‑step deployment is suggested: firstly, calculate peak simultaneous air consumption; secondly, confirm post‑treatment specifications according to dew‑point and oil‑free grade; thirdly, verify energy‑efficiency and noise data against factory test reports. Actual technical parameters shall follow the nameplate and on‑site measurement results provided by the manufacturer.
From a long‑term operational perspective, electricity expenses together with production losses caused by unexpected shutdowns usually far exceed the price gap between different equipment options. Therefore, energy efficiency and operational reliability deserve higher priority over initial procurement cost. Post‑treatment is not a simple accessory for the compressor; it determines the final compressed‑air quality. Weak links inside drainage, filtration or drying sections will degrade the whole air pipeline performance. A moderate safety margin is preferred; excessive over‑specification will raise both idle‑running energy waste and capital investment.
For continuous production lines, the efficiency advantages of variable‑frequency screw compressors become more obvious with longer daily running hours and deliver faster return‑on‑investment. For intermittent operating conditions, no‑load power waste must be carefully managed. Pipeline layout should never be overlooked. Improper pipe diameters, excessive elbows and air leakage will directly reduce end‑working pressure and compromise air purity. It is vital to close the workflow loop covering condition evaluation, proper selection and on‑site acceptance instead of simply comparing quotations.
Noise reduction should address both noise sources and propagation paths; replacing only the compressor or adding isolated enclosures alone rarely meets factory boundary noise regulations. Before placing orders, cross‑check factory test reports, official certificates and equipment nameplates. Remember that “oil‑free” does not equal “dry”. Dew‑point and residual‑oil represent two separate air‑quality dimensions and cannot substitute for each other. Filtration should adopt multi‑stage series installation from coarse filtration down to fine filtration. Complete hand‑over documentation should be properly filed to facilitate routine maintenance and trace troubleshooting.
CHANUN’s standard practice for laser‑cutting compressed‑air projects is to carry out condition assessment first and then deploy matched post‑treatment purification solutions according to required air‑quality grades.
Related news


Service Hotline: 86 13862059949
CONTACT US
Address: No.58, Dongfu Road, Suzhou Industrial Park,Suzhou, jiangsu Province, China.
Tel: (+86) 0512-62529535
WhatsApp/Wechat: (+86) 13862059949
E-mail: jiaqi.wu@chanuncompressor.com
Copyright © CHANUN 2020 All rights reserved 苏ICP备08024400号-4
www.300.cn